 EN

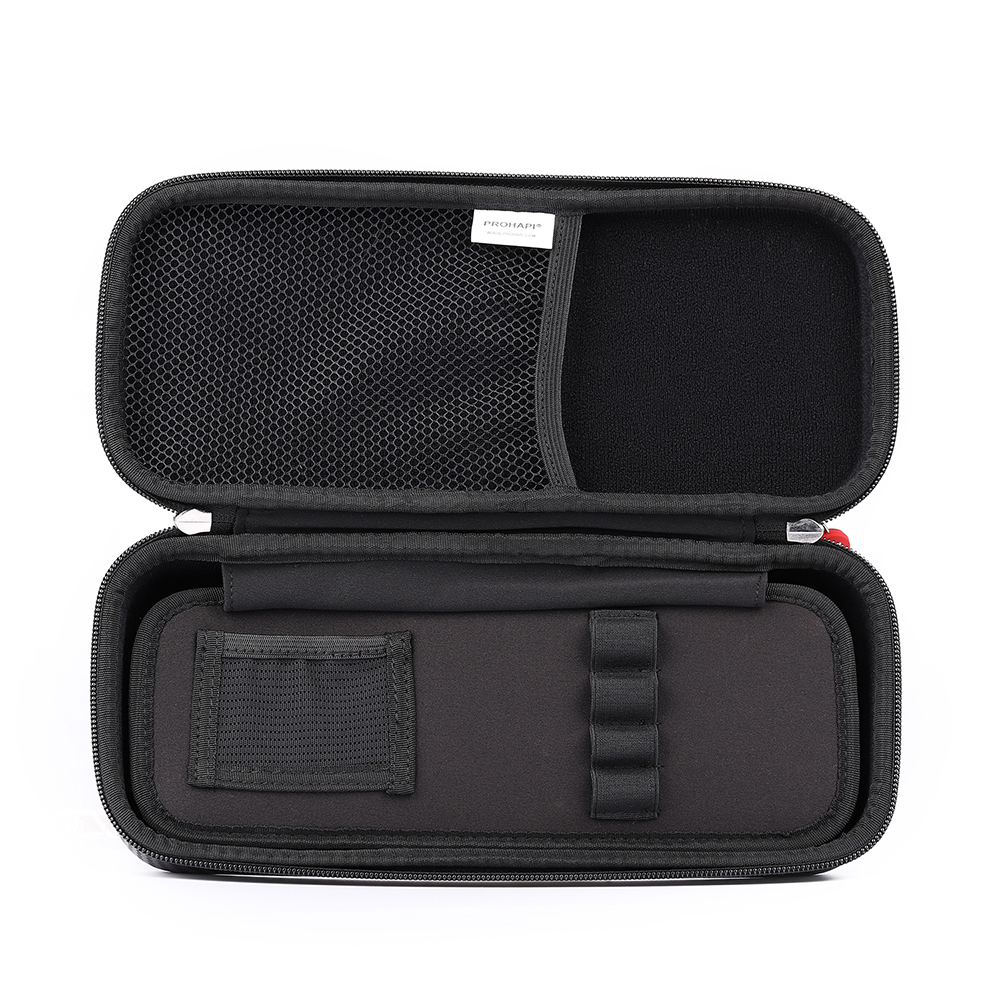
Transporting delicate equipment across global supply chains presents constant physical challenges. Diagnostic monitors, optical instruments, drone gear, and surgical kits face rough handling, sudden drops, temperature shifts, and moisture exposure. Choosing the right protective packaging determines whether a product arrives fully functional or broken.
Custom ethylene-vinyl acetate (EVA) cases offer an optimal balance of strength, shock absorption, and low weight. Combining semi-rigid structural resilience with closed-cell moisture resistance, custom EVA solutions protect sensitive equipment while remaining practical for everyday transport.
Advanced Shock Absorption and Impact Mitigation
Protection begins with kinetic energy dissipation. When a transport case hits the floor, the kinetic energy must be absorbed by the packaging rather than transferred directly to the contents inside.
Closed-Cell Foam Dynamics and Energy Dispersion
EVA cases derive their protective qualities from a dense, closed-cell foam matrix. Under impact, these microscopic sealed air pockets compress uniformly, absorbing peak force vectors and dispersing energy across the entire surface area.
Drop tests under standard shipping protocols show that custom EVA cases reduce peak acceleration forces by 50% to 60% compared to traditional hard plastic shells. Unlike expanded polystyrene (EPS) or brittle rigid plastics that crack or permanently collapse under pressure, EVA exhibits high viscoelastic recovery. It returns to its original shape after deformation, maintaining reliable protection through repeated bumps and vibration during transit.
Protecting Precision Components and Diagnostics
For sensitive diagnostic equipment and optical lenses, even subtle shocks can throw calibrations out of alignment. Precision-cut internal foam cradles each component securely, eliminating lateral movement and preventing micro-fractures during rough transit.
Environmental Defense Against Moisture and Water Ingress
Field operations rarely take place in controlled, indoor environments. Rain, high humidity, sea spray, and unexpected spills require carrying solutions that shield sensitive electronics from liquid damage.
Hydrophobic Closed-Cell Properties
Because EVA is naturally hydrophobic, its water absorption rate stays below 0.5% by weight under ASTM D570 testing standards. The material does not swell, soften, or absorb moisture, preserving interior dryness even during prolonged rainfall or high humidity.
Waterproof Seals and All-Weather Storage
When fitted with compression gaskets, tongue-and-groove sealing channels, and splash-proof zipper tracks, custom EVA cases achieve reliable IP67-rated moisture protection. Unlike fabric bags or cardboard containers that trap dampness and encourage mold growth, non-porous EVA surfaces wipe clean effortlessly and dry in seconds, preventing rust on metal tools and short circuits in electronic components.
Chemical Resistance and Long-Term Material Durability
In industrial, laboratory, and clinical settings, carrying cases regularly come into contact with harsh fluids, cleaning solutions, and environmental solvents.
Resistance to Industrial Chemicals and Solvents
EVA maintains structural integrity when exposed to dilute acids, alkalis, lubricants, oils, and common cleaning agents. Standard ISO 175 immersion tests confirm that the material resists swelling, embrittlement, and surface degradation after continuous chemical exposure.
Non-Toxic and Regulatory Compliance
Unlike PVC or lower-grade rubbers, EVA remains dimensionally stable over time without releasing plasticizer oily residue or corrosive byproducts. It naturally resists UV degradation, preventing cracking under direct sunlight. Formulated to meet strict REACH and RoHS regulatory guidelines, high-grade EVA is non-toxic, latex-free, and safe for repeated use in clinical, food-contact, and sterile environments.
High Strength-to-Weight Ratio and Handling Ergonomics
One of the biggest drawbacks of traditional heavy-duty flight cases is their excessive weight. Heavy polypropylene shells add unnecessary shipping costs and cause operator fatigue during long daily commutes.
Ultra-Low Density for Easy Mobility
EVA closed-cell foam features a density ranging between 0.1 and 0.3 g/cm³, making it up to 80% lighter than rigid plastic enclosures with similar interior volumes. Molecular cross-linking provides impressive tensile strength without requiring heavy internal metal frames or thick walls. A fully assembled case offers reliable drop protection while remaining light enough for daily field use.
Semi-Rigid Flexibility and Stackability
The semi-rigid nature of molded EVA offers a controlled elastic flex that improves grip and absorbs surface impacts without denting. High-friction exterior surface textures keep stacked cases aligned during transport, stopping gear from sliding around inside delivery vans or cargo holds. Custom-molded handles, hinges, and corner bumpers streamline ergonomics without adding loose hardware that could snap off over time.
Precision Interior Customization and Brand Presentation
A protective exterior shell reaches its full potential when paired with a custom-engineered interior layout.
Custom CNC and Water-Jet Cut Inserts
Using multi-axis CNC routing and precision water-jet cutting, internal foam inserts are shaped to match exact device contours down to fractions of a millimeter. Anti-static ESD foam variants protect sensitive circuit boards from static discharge, while multi-layered, color-coded foam layouts make missing tools immediately noticeable during inventory checks.
Exterior Branding and Custom Aesthetics
Custom EVA manufacturing supports a full suite of exterior branding techniques:
-
Deep Embossing and Debossing: Creates clean, permanent, 3D brand logos directly on the outer material.
-
High-Resolution Screen Printing: Displays vibrant corporate graphics, safety warnings, and instruction labels.
-
Custom Color Pigmentation: Matches exact corporate Pantone shades across exterior fabrics, zipper tracks, and handle grips.
Frequently Asked Questions
How does an EVA case compare to a traditional hard plastic flight case?
EVA cases offer semi-rigid impact absorption and splash resistance at a fraction of the weight of rigid plastic cases. They are far easier to carry during daily travel while still providing military-grade drop protection.
Can custom EVA cases handle marine and outdoor environments?
Yes. With an absorption rate below 0.5% and chemical resistance to salt water and UV exposure, EVA cases are ideal for marine operations, outdoor field surveys, and tropical transport.
Are custom foam inserts suitable for delicate electronic components?
Yes. Specially formulated anti-static (ESD) EVA foam inserts protect sensitive microchips and circuit boards from static discharge while providing custom shock-absorbing cavities.
How do custom EVA cases lower overall shipping costs?
Because EVA foam is up to 80% lighter than hard plastic alternatives, using EVA carrying cases significantly reduces gross freight weight, lowering shipping fees across air and ground transport routes.
Custom Packaging Solutions with EVABox
Engineering lightweight, field-ready protective cases demands specialized manufacturing equipment, precise polymer processing, and rigorous quality control. Turning raw materials into customized, durable carrying solutions requires deep industry expertise at every stage of production.
As an experienced partner in custom protective packaging, EVABox offers end-to-end design, prototyping, and manufacturing services for global companies. From 3D CAD engineering and precision thermoforming to custom CNC foam inserts and bespoke branding integration, EVABox creates custom carrying cases built to meet strict field and clinical standards. Supported by extensive manufacturing capacity and reliable supply chain networks, every project delivers uncompromised protection, sleek ergonomics, and long-term commercial value.
Table of Contents
- Advanced Shock Absorption and Impact Mitigation
- Environmental Defense Against Moisture and Water Ingress
- Chemical Resistance and Long-Term Material Durability
- High Strength-to-Weight Ratio and Handling Ergonomics
- Precision Interior Customization and Brand Presentation
- Frequently Asked Questions
- Custom Packaging Solutions with EVABox
